How to Inspect a Conveyor Belt Properly?

Time:2026-09-09 Author:Amelia
0%

Knowing how to inspect a conveyor belt properly helps prevent sudden failures, product damage, and unsafe working conditions. A belt may appear serviceable while hiding worn edges, cracked covers, or damaged internal splices. Experienced maintenance teams inspect more than the belt surface. They observe tracking, tension, pulley alignment, idlers, cleaners, and guarding. Small details matter. A frayed edge can catch on a structure. A loose fastener can become a serious hazard. Reliable inspections follow the equipment manufacturer’s instructions and the site’s approved safety procedures. Power isolation and lockout requirements must always be confirmed before hands-on work begins.

This guide explains practical inspection methods used in industrial environments. It considers what to check during operation and what requires a stopped, isolated conveyor. Look for unusual noise, material carryback, dust trails, belt drift, and fresh rubber fragments near the frame. Use a flashlight around splice zones and inspect both sides when access is safe. Record the belt’s condition with photographs, measurements, and clear notes. Guesswork is not enough. Inspection frequency should reflect load, speed, weather, belt age, and previous repair history. However, no checklist catches everything. A quiet conveyor can still contain hidden damage. That limitation deserves attention. When findings are uncertain, consult a qualified conveyor specialist rather than forcing a quick decision. Careful inspection builds dependable maintenance records and supports safer, more efficient operations.
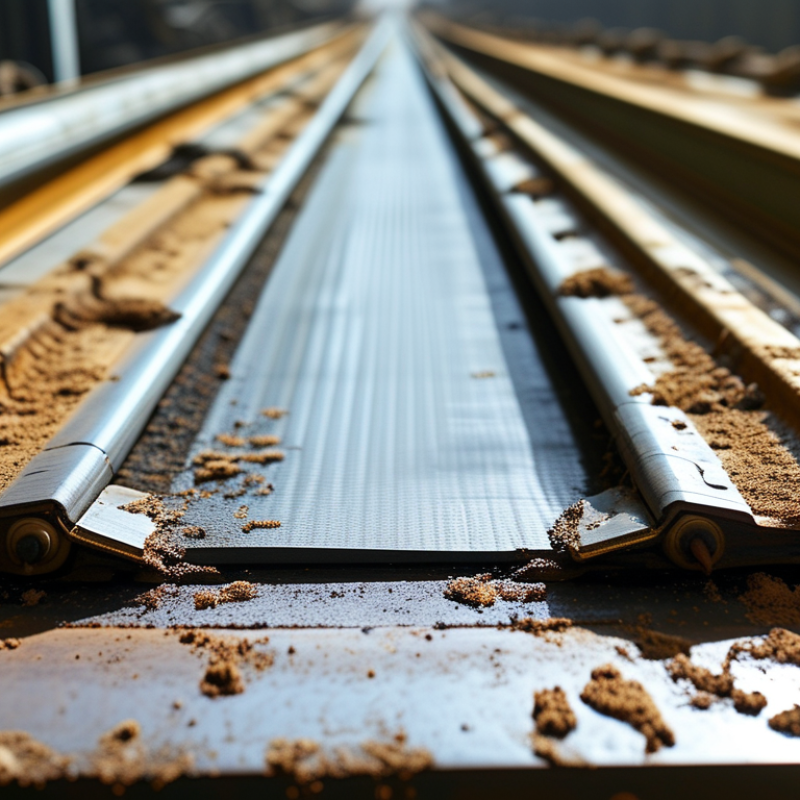
How to Inspect a Conveyor Belt Properly?

Define the Purpose and Scope of the Conveyor Belt Inspection

Before touching a conveyor, define why the inspection exists. Is it for commissioning, routine safety, failure investigation, or an audit? Each purpose changes the evidence required. Start with boundaries. Record the line ID, belt width, speed, load, transfer points, and operating hours. Include walkways, guards, pull cords, cleaners, take-up units, and emergency stops. ISO 14890:2013 provides requirements for conveyor belts, but it does not replace a site-specific inspection plan. That distinction matters.

The U.S. Bureau of Labor Statistics counted 5,283 fatal work injuries across all industries in 2023. This figure is not conveyor-specific, yet it reinforces a practical point: scope must include worker exposure, not only equipment. CEMA guidance identifies belt alignment, splice condition, guarding, and material buildup as key inspection concerns. In my field inspections, a clean running belt often hides a damaged splice. Watch the loaded belt, not only the stopped belt. Observe carryback, mistracking, unusual noise, and access behavior during normal production.

Define acceptance limits before collecting findings. For example, classify defects as immediate shutdown, scheduled repair, or observation. Photograph the exact location, direction, and operating condition. Do not guess. I once treated a small edge cut as cosmetic; repeated flexing enlarged it within days. The inspection scope should also state what it cannot verify, such as internal carcass damage without specialized testing. Revisit that limitation during the next review.

Prepare Safety Measures and Required Inspection Tools

A conveyor belt inspection begins with controlled conditions, not a quick glance. Stop the conveyor, isolate every energy source, and apply the site’s lockout and tagout procedure. Confirm that the belt cannot move before approaching it. Wear safety glasses, protective gloves, hearing protection, and footwear with good traction. Loose clothing must stay away from rollers and pulleys. Keep another trained person nearby when access is difficult.

Use a bright flashlight to examine belt edges, splice lines, covers, and the underside. A steel ruler helps measure tears, edge separation, and unusual gaps. Use a belt gauge to check thickness loss at several points, not just the damaged area. A tape measure can record tracking changes and pulley alignment. An infrared thermometer may reveal a hot bearing or slipping belt after controlled operation. Record each reading with the location and inspection time.

Small details often explain larger failures. Look for trapped stones, exposed cords, cracked lagging, and material packed around return rollers. I once focused too heavily on surface cuts and missed a misaligned support frame. That mistake changed my inspection routine. I now check the belt path before judging the belt itself. Conditions can also mislead inspection results. Dust may hide a splice defect, while rain can make abrasion look worse. Clean only when the equipment is safely isolated, and never rely on memory alone. Photographs and consistent measurements make maintenance decisions more reliable.

How to Inspect a Conveyor Belt Properly? - Prepare Safety Measures and Required Inspection Tools
Inspection Stage Inspection Point What to Check Required Tool or Equipment Potential Risk Recommended Frequency Acceptable Condition and Corrective Action
Safety Preparation Energy isolation Confirm that electrical, pneumatic, hydraulic, and stored mechanical energy sources are isolated before accessing moving parts. Lockout/tagout devices, isolation checklist, voltage tester High Before every hands-on inspection Equipment remains locked and tagged until the inspection is complete and all personnel are clear.
Safety Preparation Personal protective equipment Verify the use of safety footwear, eye protection, suitable gloves, hearing protection, and high-visibility clothing where required. Site PPE checklist High Before entering the inspection area Required PPE is correctly worn and free from visible damage. Replace damaged or unsuitable PPE.
Safety Preparation Guards and emergency devices Check that nip-point guards, pull-cords, emergency-stop devices, warning signs, and access gates are present and unobstructed. Visual inspection checklist, functional test procedure High Daily visual check; functional test according to site procedure All guards are secure and emergency devices operate correctly. Stop use and repair missing or defective protection.
Visual Inspection Belt surface Look for longitudinal cuts, transverse cracks, punctures, gouges, frayed edges, exposed reinforcement, hard spots, and material buildup. Inspection light, camera, cleaning brush, straightedge High Daily or before each operating shift The belt surface is free from damage that could spread or expose reinforcement. Remove buildup and schedule repair or replacement when defects are found.
Visual Inspection Belt edges Inspect both edges for curling, splitting, abrasion, cuts, and contact with the conveyor structure. Inspection light, measuring tape Medium Weekly and after a tracking incident Edges run clear of the structure. Correct tracking and repair edge damage before it becomes extensive.
Visual Inspection Splice condition Examine mechanical fasteners or vulcanized joints for separation, lifted edges, missing fasteners, looseness, and unusual wear. Inspection light, ruler, torque wrench where applicable High Weekly and after overload or belt impact The splice is even, secure, and free from separation. Remove the belt from service if the splice threatens safe operation.
Alignment Check Belt tracking Observe whether the belt remains centered on the pulleys and idlers during empty and loaded operation. Visual observation, measuring tape, tracking record sheet Medium Daily during operation The belt does not consistently contact the structure. Investigate loading, idler alignment, material buildup, and tension if mistracking occurs.
Alignment Check Idlers and return rollers Check for seized, noisy, damaged, misaligned, or unevenly rotating rollers and verify that frames are secure. Inspection light, non-contact temperature meter, listening inspection Medium Weekly; more often in dusty or abrasive service Rollers rotate smoothly without abnormal heat or noise. Replace seized or damaged components promptly.
Mechanical Inspection Pulleys and lagging Inspect pulley shells, shafts, bearings, and lagging for wear, cracks, material buildup, looseness, or abnormal movement. Inspection light, straightedge, non-contact temperature meter, vibration meter High Monthly and after abnormal vibration Surfaces are intact and components run without excessive heat or vibration. Isolate the conveyor before repair.
Mechanical Inspection Belt tension Check for excessive slack, over-tension, slipping, or signs that the take-up system has reached its adjustment limit. Belt tension gauge, measuring tape, manufacturer-approved procedure Medium Monthly and after splice or belt replacement Tension is within the equipment’s specified operating range. Adjust only according to the approved maintenance procedure.
Cleaning and Loading Skirting and loading zone Inspect skirt rubber, impact beds, loading chutes, and transfer points for wear, blockage, spillage, or belt contact. Inspection light, scraper, measuring tape, cleaning tools Medium Daily in high-spillage applications Material is contained without excessive friction or belt damage. Clean safely and adjust or replace worn sealing components.
Cleaning and Loading Belt cleaners and scrapers Check blade wear, mounting security, alignment, pressure, and accumulation of carryback on the return side. Inspection light, ruler, hand tools Medium Weekly Cleaner contact is even and does not damage the belt. Replace worn blades and remove trapped material after isolation.
Operational Check Noise, vibration, and temperature Identify unusual noise, vibration, overheating, burning odor, belt slip, or motor and gearbox irregularities. Vibration meter, non-contact temperature meter, sound observation record High Daily while operating Readings and operating behavior remain stable. Stop and investigate any rapid change or abnormal condition.
Operational Check Start-up and shutdown sequence Verify that alarms, interlocks, start-up delays, emergency stops, and shutdown procedures function as intended. Control-panel checklist, communication device, approved test procedure High At scheduled intervals defined by site procedures Controls respond in the correct sequence and personnel receive adequate warning. Remove the conveyor from service if a safety function fails.
Documentation Inspection records Record inspection date, conveyor identification, operating condition, defects, measurements, photographs, assigned action, and completion date. Inspection form or digital maintenance system, camera Low Every inspection Records are complete, traceable, and reviewed by a responsible person. Escalate overdue high-risk actions immediately.

Examine the Belt Surface, Edges, Splices, and Covers

How to Inspect a Conveyor Belt Properly?

A reliable inspection begins with the belt surface. Stop and isolate the conveyor before touching it. Look for longitudinal cuts, transverse cracks, abrasion, blisters, and exposed reinforcement. A polished strip may indicate belt slip, not normal wear. Measure damaged areas with a ruler and record their location. The CEMA Belt Conveyors for Bulk Materials handbook recommends tracking belt alignment, loading, and wear trends instead of relying on one visual check. Dust can hide small defects. Wipe a safe section carefully, then inspect again.

Inspection focus Longitudinal cuts Transverse cracks Abrasion and blisters Exposed reinforcement

Examine both edges for curling, fraying, and impact damage. Uneven edges often reveal mistracking or poor loading. Check every splice for lifted rubber, loose fasteners, gaps, and hardness changes. A splice may look acceptable from above but fail along its underside. Inspect the top and bottom covers separately. Compare cover thickness with the original specification in ISO 14890. Even a small reduction deserves documentation. I sometimes expect a clean belt to be healthy, but that assumption is unreliable.

Tips: Use a flashlight, inspection gauge, camera, and written checklist. Mark defects with removable chalk. Photograph the same points each shift. Compare measurements, not impressions. If cracks grow between inspections, reduce the inspection interval and involve a qualified belt technician. Keep people clear of stored tension energy. Never test a moving belt by hand. Poor lighting remains an easy mistake.

Inspect Conveyor Components and Identify Signs of Wear

How to Inspect a Conveyor Belt Properly?

Inspect Conveyor Components and Identify Signs of Wear

Before examining the conveyor, isolate its power according to site procedures. Walk along the entire belt, not just the loading area. Look for edge fraying, longitudinal cuts, blisters, exposed fabric, and uneven belt thickness. Run a gloved hand near damaged areas only when the belt is stopped. A small crack can expand quickly under tension. Check splice plates or vulcanized joints for lifting edges, gaps, and unusual stiffness.

Inspect idlers for seized bearings, flat surfaces, and rattling sounds. Examine pulleys for worn lagging, material buildup, and misalignment. Scrapers should contact the belt evenly without gouging it. Watch the belt during a controlled test run. Persistent drifting often indicates poor tracking, uneven loading, or a distorted frame. Measure belt sag and record temperatures near bearings. A simple photo log helps compare changes between inspections.

Tips: Use a flashlight and inspection mirror. Mark defects with location and date. Compare readings with previous records. Do not ignore dust patterns; they may reveal hidden friction. A rushed inspection can miss serious wear. I have learned that clean-looking belts may still hide damaged splices. Recheck questionable areas after cleaning, and ask another technician to review uncertain findings.

How to Inspect a Conveyor Belt Properly?

Inspect the belt, splices, idlers, pulleys, cleaners, and tracking system for visible damage, abnormal noise, material buildup, and alignment problems. The chart shows the relative number of inspection points commonly used in a complete conveyor inspection.

A higher value indicates more inspection points to verify because the component can affect belt safety, tracking, and service life.

Record Findings and Plan Corrective Maintenance Actions

How to Inspect a Conveyor Belt Properly?

A proper inspection must produce more than a list of defects. It should create a clear maintenance plan. Before inspection, isolate the conveyor under site-approved energy-control procedures. Check the belt surface, splice, pulley lagging, idlers, cleaners, guards, and emergency-stop devices. Look for edge fraying, mistracking, trapped material, unusual heat, and loose fasteners. Record the exact location, defect size, operating condition, and inspection time. Photographs help, but measurements are stronger evidence.

The U.S. Bureau of Labor Statistics reported 1,495 fatal work injuries in transportation and material-moving occupations during 2023. That figure is not conveyor-specific, but it shows why weak inspection records can create serious exposure. Assign each finding a risk level and an owner. Critical defects need immediate isolation or controlled repair. Minor wear can enter a scheduled work order. Include spare parts, labor, access requirements, and a target completion date. Then verify the repair after the belt runs. A closed work order is not proof of a corrected hazard.

Tips: Use one consistent inspection form. Mark defects with belt distance or pulley reference points. Record photos from the same angle. Compare readings over time. Do not trust appearance alone. A belt may look acceptable while its splice is weakening. Also, inspection intervals should reflect dust, load, speed, weather, and past failures. A fixed monthly schedule may be convenient, but sometimes it is simply wrong. Review it.

FAQS

: Why should a conveyor belt inspection have a defined purpose?

: The purpose determines what evidence you need. It may support commissioning, routine safety, failure review, or an audit. Set clear boundaries before inspecting.

What equipment details should the inspection record?

Record the line ID, belt width, speed, load, transfer points, and operating hours. Include walkways, guards, pull cords, cleaners, take-up units, and emergency stops. Worker exposure matters too.

What should be observed during normal operation?

Watch the loaded belt, not only the stopped belt. Look for mistracking, carryback, unusual noise, and unsafe access behavior. A clean belt can hide a damaged splice.

How should the belt surface be checked?

Isolate the conveyor before touching it. Inspect for longitudinal cuts, transverse cracks, abrasion, blisters, and exposed reinforcement. Use a ruler to measure damaged areas. Dust can hide defects.

What do belt edges and splices reveal?

Check edges for curling, fraying, and impact damage. Uneven edges may indicate mistracking or poor loading. Inspect each splice from above and below. Look for lifted rubber, loose fasteners, gaps, and hardness changes.

How can belt wear be documented accurately?

Compare cover thickness with the original specification. Photograph fixed locations under similar conditions. Use a flashlight, inspection gauge, camera, and written checklist. Measure defects instead of relying on impressions.

How should inspection findings be classified?

Define acceptance limits before collecting evidence. Classify defects as immediate shutdown, scheduled repair, or observation. Record the exact location, direction, and operating condition. Do not guess.

What limitations should inspectors acknowledge?

Visual checks may not verify internal carcass damage. Specialized testing may be required. I once dismissed a small edge cut as cosmetic. Repeated flexing enlarged it within days. That mistake deserves review.

Conclusion

A proper conveyor belt inspection begins by defining its purpose and scope, including the belt’s operating conditions, inspection frequency, and areas that require special attention. Before starting, shut down and isolate the conveyor according to site safety procedures, use appropriate protective equipment, and prepare essential tools such as a flashlight, measuring device, inspection mirror, and note-taking materials. A clear plan helps ensure that no critical area is overlooked.

To understand how to inspect a conveyor belt properly, examine the belt surface, edges, covers, and splices for cuts, cracks, fraying, deformation, exposed reinforcement, or separation. Inspect rollers, pulleys, cleaners, frames, bearings, and tracking systems for unusual noise, misalignment, looseness, corrosion, and excessive wear. Record each finding with its location, severity, and possible cause. Finally, prioritize corrective actions, schedule repairs or replacements, and arrange follow-up inspections to confirm that the conveyor remains safe, reliable, and efficient.

Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......